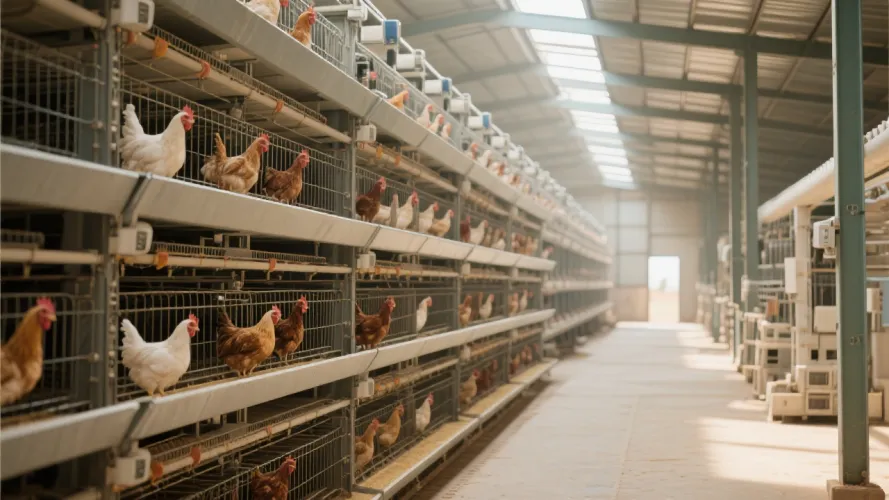
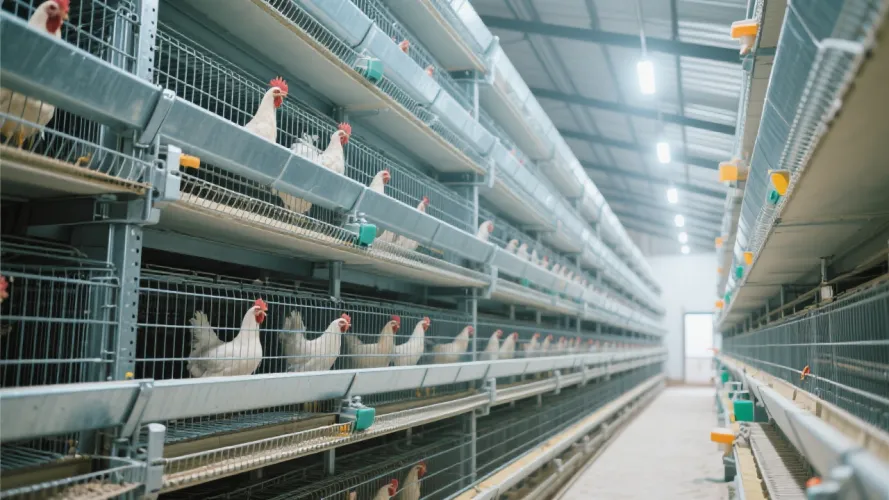
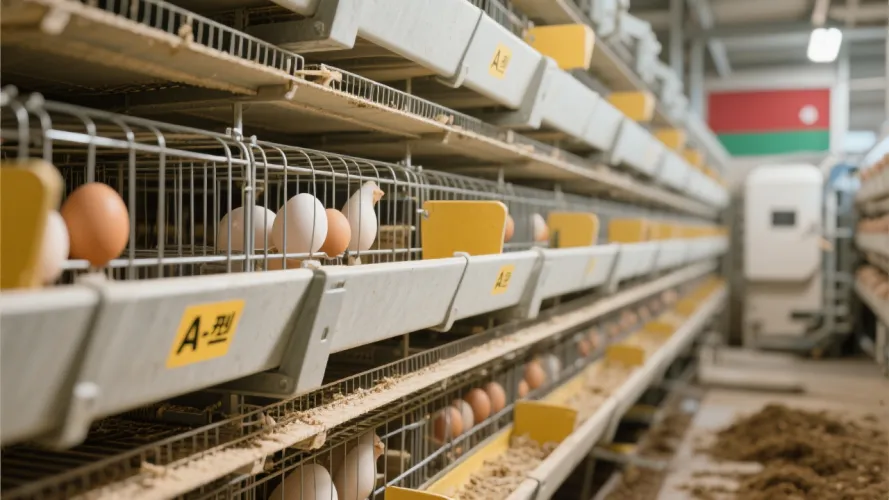
A customer in Mongolia selected the Livi H-Type Automatic Layer Cage System for a 15,000 layers poultry farm project. The farm adopts fully automated feeding, egg collection, manure removal, and ventilation systems to improve production efficiency and prepare for future farm expansion.
If you are planning to build a 30000 layers poultry farm in Zambia, choosing the right equipment is critical for improving egg production, reducing labor costs, and ensuring stable farm management.
This customer case study reviews how large-scale broiler farms ranging from 10,000 to 50,000 birds improved daily management efficiency and space utilization through a science-based housing plan. The featured solution centers on H-type broiler battery cages manufactured with Q235 steel and protected by hot-dip galvanizing to enhance corrosion resistance and service life in demanding farm environments. By applying a multi-tier cage layout, the farms streamlined routine work such as feeding, observation, and flock handling while building a more standardized production workflow suited to scale-up operations. The article summarizes practical implementation insights, measurable management improvements, and real customer feedback to help decision-makers evaluate suitability for their own sites. It also outlines end-to-end support—from solution design and equipment preparation to transportation guidance and on-site installation—so farms can plan with greater confidence and adopt a tailored approach for stable, efficient broiler production.
This news article reviews three real-world large-scale broiler operations raising 10,000, 30,000, and 50,000 birds, and explains how they improved productivity and management efficiency by adopting Zhengzhou Livi Machinery Manufacturing Co., Ltd.’s customized H-type broiler battery cage solution. It highlights key advantages such as Q235 bridge-grade steel construction, hot-dip galvanized anti-corrosion treatment for long service life, and multi-tier cage design that increases space utilization while simplifying daily routines. Supported by before-and-after operational comparisons and customer feedback, the cases demonstrate how standardized equipment design, streamlined management, and reliable logistics/installation support can help large farms strengthen competitiveness and achieve higher overall farming returns at scale.
This news feature analyzes three real-world large-scale broiler operations—10,000, 30,000, and 50,000 birds—to show how optimized housing and management can drive measurable productivity gains. Through these case studies, the article highlights how an H-type broiler battery cage solution from Zhengzhou Livi Machinery Manufacturing Co., Ltd. improves space utilization, standardizes daily routines, and strengthens long-term investment security. Key technical advantages include Q235 bridge steel construction and hot-dip galvanized anti-corrosion treatment to extend service life, plus multi-tier structural design that supports smoother flock handling and more efficient farm workflows. The article also explains end-to-end project support such as logistics coordination and on-site installation guidance, and uses before-and-after comparisons and customer feedback callouts to illustrate practical performance improvements. Written in a clear, story-driven style for decision-makers, it helps large-scale farmers evaluate cage-based broiler systems and plan a scalable, efficiency-focused upgrade.
A poultry farm in Ghana, striving to enhance the quality of its eggs and improve farming efficiency, introduced the high-performance A-type battery cage from Zhengzhou Livi Machinery Manufacturing. This cage is made of hot-dip galvanized Q235 steel and offers options of 3 to 5 tiers with customizable capacities. Equipped with automation features, the farm reported that egg production during peak laying periods exceeded 90%, significantly boosting egg quality, which in turn earned the farm an outstanding reputation. This successful experience serves as a guiding light for poultry practitioners across Africa seeking to elevate their operations.
In the global poultry industry, space efficiency is a key driver of profitability. This case-driven analysis explores how Zhengzhou Livi Machinery’s innovative H-frame layer cage system boosts hen density per square meter—from 5,000 to 30,000 birds—while improving ventilation, reducing labor costs, and enhancing animal welfare. Real-world data from farms across China and Southeast Asia show up to 40% higher stocking capacity, 25% lower labor input, and reduced disease incidence due to optimized layer spacing. Integrated automation for egg collection and manure removal, combined with ISO9001, ISO14001, and CE certifications, ensures durability, safety, and compliance. Whether you're managing a small farm or scaling up, this guide helps you evaluate whether an H-frame cage solution aligns with your operational goals—and what to consider before making the switch.
Discover the secrets behind the quality improvement in Ghana’s poultry farms! This farm has introduced the high-efficiency Type A layer chicken battery cage manufactured by Zhengzhou Livi Machinery. Made of hot-dip galvanized Q235 steel, these cages are robust and durable, with customizable options available in 3 to 5 tiers. Featuring automation capabilities, the farm has seen an egg production peak exceeding 90% during the laying season, leading to a remarkable enhancement in egg quality. This transformation has earned a stellar reputation in the market.
This article narrates the impressive transformation of a poultry farm in Zambia, transitioning from traditional farming methods to an efficient, smart farming approach. The farm implemented the high-efficiency A-type layer chicken battery cages from Zhengzhou Livi Machinery Manufacturing Co., Ltd., featuring automated feeding, manure cleaning, and egg collection capabilities. Post-upgrade, the farm has seen an increase in egg production rates and a significant reduction in labor costs. Additionally, this product has garnered numerous satisfied customers in countries such as Nigeria, Kenya, and South Africa, making it a valuable reference for other poultry operations.
This case study explores the successful application of Zhengzhou Livy Machinery’s high-efficiency H-type layer chicken cages in international egg production operations. Focusing on modern poultry farm design and operational strategies, it highlights how the H-shaped structure maximizes space utilization while enabling automated feeding, egg collection, and cleaning systems—reducing labor costs significantly. The article emphasizes the critical role of ventilation and temperature control in maintaining flock health and boosting egg output, supported by real-world data from overseas farms. It also guides producers of varying scales on selecting appropriate equipment capacity and implementing preventive maintenance for long-term efficiency and sustainability. Backed by ISO9001, ISO14001, and CE compliance standards, this comprehensive analysis offers actionable insights for global poultry operators seeking green, scalable solutions. A soft introduction to Livy Machinery’s cage system and technical support services concludes the piece, encouraging consultation for optimized farm performance.
Discover how a 5000-hen commercial egg farm achieved measurable operational improvements through the integration of H-type layer cage systems featuring automated manure removal and egg collection. This case study details real-world outcomes—including a 35% reduction in labor costs, an 8% increase in egg production, and doubled waste management efficiency—while enhancing flock health. With structured data comparisons, system design insights, and customer testimonials, this guide offers a replicable path for modernizing medium-scale poultry operations toward intelligent, sustainable farming.
Discover how a poultry farm in Henan, China, achieved significant reductions in labor costs and improved egg production efficiency after implementing automated manure removal and egg collection systems. This real-world case study explores the H-type layer cage design’s role in solving traditional farming challenges—labor intensity, hygiene risks, and low productivity—and demonstrates measurable outcomes for medium-to-large-scale operations (5,000–30,000 hens). Ideal for farm managers seeking to transition from manual to intelligent poultry farming.
Discover the key automation functions of A-type layer cages by Livi Machinery, including automatic feeding, manure removal and egg collection, that elevate hygiene, efficiency and management in poultry farms.
Learn the essential first steps for starting a poultry farm, including choosing the farming direction, assessing budget and scale, confirming sales channels, planning the poultry house and selecting equipment with Livi Machinery.
Discover how Livi Machinery supports 20,000-layer poultry farm projects with site planning, customized 3–5-tier A-type layer cage solutions, equipment production, delivery and project implementation guidance.
READY TO START?
Ready to Build Your Poultry Farm?
Tell us your land size, poultry type and farming capacity. LIVI will provide a complete farm solution for your project.